When a food, pharmaceutical or cosmetics package suddenly “draws air” on the retail shelf, the modified atmosphere escapes, liquids leak out or the product spoils long before its best-before date, the search for the cause usually begins in earnest. Very often, suspicion falls immediately on the barrier of the film: “The oxygen barrier isn’t good enough!” But after more than 30 years of laboratory practice at Innoform Testservice and countless failure analyses, I can assure you that in the vast majority of cases, the film web is not the problem – the seal is.
Around 90% of all flexible consumer packaging today is heat-sealed using thermal contact processes. The seal is the structural Achilles’ heel of every flexible package. This is exactly where material properties, machine settings, tool geometries and the product being filled come together within fractions of a second. In this detailed technical article, drawing on scientific market studies (including those by OFI in Vienna and Fraunhofer IVV / IVLV), our seminar materials and our accredited testing practice, I will show you how many film packages actually suffer from sealing problems, why tiny capillaries undermine even the best high barrier, and how you can reliably avoid typical leaks through smart testing and sound know-how.
How many film packages leak because of sealing problems? A look at the OFI study and the market
At the start of our seminars, I like to ask a provocative question: “How many modified atmosphere or vacuum packs on the supermarket shelf do you think are not actually as leak-tight as the brand owner believes?” Participants’ answers usually lie at a cautious 0.1 to 0.5 per cent – after all, modern packaging lines are highly automated. The scientific data, however, paint a far less flattering picture.
The well-known market study by OFI in Vienna
A comprehensive investigation by the Austrian Research Institute for Chemistry and Technology (OFI) in Vienna (led by Dr. Michael Washüttl, Prof. Manfred Tacker and Birgit Tauschitz) is particularly revealing in this respect. In the German-speaking region (D-A-CH), OFI examined a total of more than 1,600 foods packed under modified atmosphere (MAP – Modified Atmosphere Packaging) from regular retail – including meat and sausage products, cheese, fish, bakery products and convenience foods. In addition, a specific sample of 386 modified atmosphere packs from German retail was examined in detail.
The result caused a stir throughout the entire packaging industry:
- Only 56% of all MAP packs examined had an optimal modified atmosphere at retail.
- approx. 33% up to as much as 44% of the packs – and in the German retail sample even almost 50% – showed significant deficiencies in the gas mixture or did not fulfil their intended purpose of extending shelf life.
- Besides an incorrectly designed film barrier and interactions between the packed product and the test gas, the Viennese researchers identified the main causes above all as leaks due to defective seals: unsuitable sealing tools, misadjusted or incorrectly reading temperature sensors on the sealing jaws, mechanical overstressing during packing and product contamination in the seal area.
Complementary studies by WRAP and IVLV / Fraunhofer IVV
These findings are fully consistent with other international surveys. A widely cited British study by the organisation WRAP (“Seal integrity and the impact on food waste”, Dudbridge & Turner) and IVLV Information Sheet No. 114 from the research project EVOCOSEAL (Fraunhofer IVV in cooperation with Hasselt University and KU Leuven) show impressively that:
- In 58% of all cases of defective packaging, contamination of the seal (by product splashes, fats, dusts or condensate) is the primary cause of pack failure.
- Depending on the film type and contamination, product residues in the seal area can cause seal strength to drop by up to 88%.
Even though these studies date back a few years, the trend remains unbroken today. Sealing problems are still the main cause of leaks in flexible packaging.
My practical estimate: How many packs are really affected today?
Of course, inline quality control has evolved since the first OFI surveys. Obvious “bursts” or completely open seals that are immediately noticed on the filling line are usually in the range of 0.1 to 1% at well-run plants. But that is only half the truth – because a large proportion of critical leaks consist of micro-leaks (capillaries 10 to 50 µm in diameter) at fold transitions or of a pre-damaged hot seal (hot tack), which often go undetected in a quick spot check in a water bath or only open up during transport as a result of pressure and vibration stresses.
If we combine the findings of OFI Vienna, the Fraunhofer/IVLV research and our ongoing laboratory tests at Innoform Testservice, my realistic estimate for today’s market is as follows:
- 70 to 80% of all real-world package leaks do not originate in the intact film surface, but directly in or immediately next to the seal (seal edges, gussets, 2-/4-ply transitions).
- Across all flexible film packaging at retail, an estimated 3 to 8% of all packs have avoidable seal weaknesses or micro-leaks.
- For sensitive MAP packs, vacuum packs, liquid and powder products, as well as on lines recently converted to mono-materials or paper-based laminates, the rate of seals that are not optimally leak-tight is in practice often as high as 5 to 15%.
“Barrier begins where leak tightness ends. Before philosophising about permeation, everything has to be tight first.”
Barrier vs. leak tightness: why a single 25 µm hole renders any high-barrier film package useless
To understand why even the smallest sealing defects have such dramatic consequences for product protection, it is worth looking at a simple calculation that I regularly work through in our seminar “Leak Testing, Sealing and Processing of Barrier Film Packaging (Barrier Films Part 4 (in German))”.
Imagine a classic high-barrier pouch with a surface area of 375 cm², made from a metallised laminate (PET-BO met. 12 µm / PE 90 µm). The oxygen transmission rate (OTR) of this intact barrier film is an excellent 0.3 cm³/(m² · d · bar):
- Oxygen ingress through permeation (intact film area): Across the entire pouch area of 375 cm², with a pure oxygen gradient, only 0.011 cm³ of oxygen per day per pack diffuses through the material.
- Oxygen ingress through a single micro-leak in the seal: Now let us assume that a tiny crease or a dust particle has created a single continuous capillary (“channel”) with a diameter of just 25 µm (half the thickness of a human hair!) in the 10 mm wide seal. Through this one micro-channel alone, around 0.052 cm³ of gas flows into the pack every day.
In plain terms: a single 25 µm capillary in the seal lets almost five times as much oxygen into the package as the entire high-barrier film put together! And if the pore diameter is 50 µm, gas ingress multiplies drastically once again. Anyone who spends a lot of money on EVOH, SiOx, AlOx or aluminium barriers but does not have their seals under control is simply throwing money out of the window.
“How tight is tight?” – Typical defects and leak rates
Absolute leak tightness in the physical sense does not exist – what matters is always which defect size becomes critical for your specific product. The following overview (based on guide values from the Fraunhofer Institute IVV and leak measurement technology) helps with practical classification:
| Everyday requirement | Critical pore size / capillary diameter | Typical leak rate (guide value) | Practical example & risk |
|---|---|---|---|
| Sift-proof / insect-proof | approx. 100 – 200 µm | > 10⁻¹ mbar·l/s | Sugar, flour, rice; protection against stored-product pests |
| Dust-tight | approx. 25 – 30 µm | approx. 10⁻¹ to 10⁻² mbar·l/s | Fine powders, spices, cocoa powder |
| Water-vapour-tight | approx. 20 – 25 µm | approx. 10⁻² mbar·l/s | Dry products, crackers, milk powder clumping |
| Liquid-tight (droplets) | approx. 15 – 20 µm | approx. 10⁻² mbar·l/s | Soups, sauces, pet food, wet wipes |
| Vapour-tight (“sweating”) | approx. 10 – 15 µm | approx. 10⁻³ mbar·l/s | Aroma loss, drying out during storage |
| Gas-tight & bacteria-tight | approx. 5 – 10 µm | approx. 10⁻⁴ mbar·l/s | MAP packs, vacuum packs, medical devices |
The 5 typical causes of leaking seals – and how to avoid them
When customers from the food, pharmaceutical or consumer goods industries send rejected pouches or trays to our laboratory in Oldenburg, our failure analysis repeatedly uncovers five recurring failure patterns. The good news: each and every one of these problems can be reliably eliminated with the right choice of materials and targeted testing.
1. Contamination in the seal area (“sealing through contamination”)
When pouches and trays are filled, cocoa powder, ground coffee, milk powder or grated cheese gets stirred up; with moist products, marinades, fats, cooking oils or condensation splash onto the seal area. If this product gets between the sealing jaws, it acts as a release layer and prevents the molten polymer chains from interdiffusing (entangling).
How to avoid this defect: Besides optimised product dosing and extraction, the decisive factor here is above all the sealant layer. While simple standard PE-LD or PP-BO quickly reaches its limits when contaminated, low-melting metallocene polyethylenes (mLLDPE), ethylene copolymers (such as EVA) or ionomers (known e.g. as Surlyn®) can “flow around” dust particles and the finest grease films much better thanks to their low melt viscosity and still seal tightly.
2. The critical 2-to-4-layer transition (side gussets, overlaps and “gussets”)
Take a close look at a typical flow wrap pouch (flowpack) or a stand-up pouch (doypack): where the longitudinal seal (fin seal) or the side gusset runs into the cross seal, the material thickness jumps abruptly from two layers to four layers. Precisely at this edge, a small wedge-shaped cavity forms – the so-called gusset.
If the sealing layer is designed too thin (e.g. only a few micrometres of heat-sealable coex PP) or the sealing jaws are rigid and incorrectly profiled, the volume of molten polymer is simply insufficient to “flood” this step. A continuous capillary channel of 20 to 100 µm remains open.
How to avoid this defect: The thickness and flowability of the sealing layer must always be matched to the total thickness of the laminate and the step height. Using a microtome cross-section under the light microscope in combination with a dye penetration test according to DIN 55508-2, we can make visible in our laboratory within a very short time whether the gusset is cleanly filled or whether polymer mass is missing.
3. Insufficient hot seal strength (hot tack failure)
On high-speed vertical form-fill-seal machines (VFFS), the following happens: the cross jaws seal the bottom seam, open, and just milliseconds later the heavy product (e.g. 500 g of nuts, frozen vegetables or washing powder) drops from the forming tube directly onto the still hot, molten seal. At the same time, the film draw-off pulls on the seal.
If the sealing layer has too weak a hot tack (hot seal strength) in this hot temperature window, the melt is partially pulled apart. Fine strings, micro-cavities or local tears form. The insidious part: if you later test the cooled pouch in a standard tensile test, the seal still appears to be strong – but due to the micro-channels drawn while hot, the pouch has long since been leaking!
How to avoid this defect: In high-speed FFS processes, never rely solely on the cold seal strength. Have a complete hot tack curve according to DIN 55571-2 or ASTM F 1921 recorded. It shows exactly at which sealing temperature the material offers the highest resistance in the hot state.
4. Narrower sealing windows due to mono-materials and paper laminates (PPWR effect)
In the past, classic laminates such as PET/PE or OPA/PE were extremely forgiving: the outer PET or PA layer only melted beyond 220 to 250 °C, while the inner PE layer already sealed from 105 °C. The machine operator had a comfortable sealing window of 30 to 50 °C. If the seal did not hold, you simply turned up the temperature on the machine by 15 degrees – and it ran.
With the European Packaging and Packaging Waste Regulation (PPWR) and the switch to recyclable all-PE or all-PP mono-materials as well as to fibre-based barrier papers with ultra-thin dispersion sealing coatings, this picture has completely reversed:
- With polyolefin mono-materials, the melting points of the outer layer (e.g. oriented BOPE or BOPP) and the inner layer (sealant PE or sealant PP) are close together. If sealing is too hot, the outer film shrinks, the seal warps into waves or the molten polymer is squeezed out at the edge of the sealing jaw – resulting in a thin spot and a classic seal edge fracture.
- With paper laminates, the paper acts as a thermal insulator (poor heat transfer), while the inner dispersion coating is often only a few grams per square metre thin and can barely compensate for unevenness in the paper fibres.
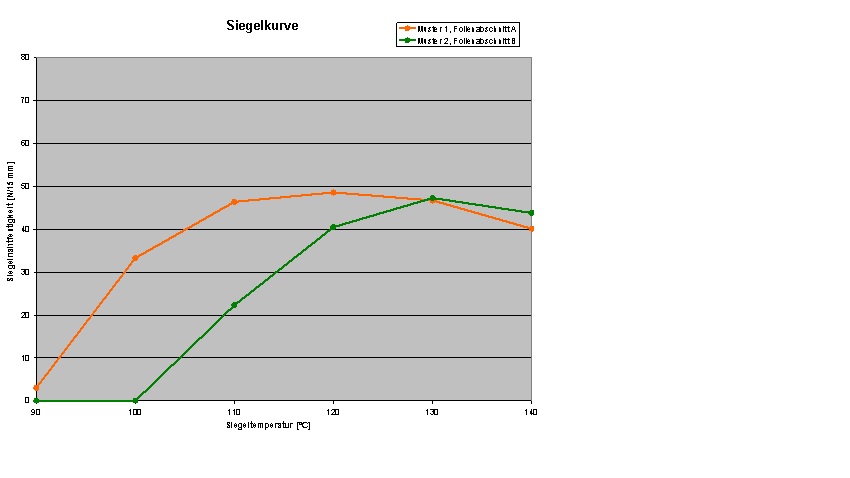
How to avoid this defect: As the diagram from one of our sample laboratory reports shows, even a slight change in the coextrusion formulation (e.g. a lower proportion of low-melting plastomer in the PE blend) can shift the seal initiation temperature (SIT) upwards by 10 to 15 °C. By combining a laboratory sealing curve (DIN 55529), DSC melting point analysis and FTIR spectroscopy, we determine beyond doubt whether the material has deviated or whether the temperature distribution of your sealing jaws needs to be readjusted.
5. The trade-off between leak tightness and easy opening (peel seals)
Consumers want packaging that can be opened smoothly by hand without scissors (easy peel) – while quality assurance demands absolute leak tightness throughout the entire logistics chain. A widespread misconception is: “A peel seal with 4 N/15 mm is less tight than a lock seal with 40 N/15 mm.”
Physically, this is not true: as long as the sealing layer is continuously sealed through, a peel seal (whether adhesive peel, cohesive peel via incompatible blends such as polybutene-1, or delamination peel) is just as gas- and liquid-tight as a lock seal. It only becomes critical when external forces – such as the post-tensioning of a vacuum pack, the rise in internal pressure during lorry transport over an Alpine pass, or impacts inside the carton – exceed the peel initiation force of the seal and the seal partially “creeps open”.
How to avoid this defect: In addition to the pure strip tensile force, also test the actual opening forces on the complete package according to DIN 55409-1 (flexible packaging) or DIN 55409-2 (rigid trays), and specifically match the sealing jaw contour (e.g. a rounded profile for gentle peel initiation) to your peel system.
Testing correctly at Innoform Testservice: systematically safeguarding seal strength and leak tightness
In our test laboratory in Oldenburg, accredited to DIN EN ISO/IEC 17025 (DAkkS), we make a strict distinction between two complementary testing pillars: mechanical seal tests (How high is the holding force and how wide is the process window?) and physical leak tightness tests (Are there any continuous channels or pores?). Both are inseparable parts of a sound packaging specification.
Pillar 1: Testing seal strength, sealing curves and hot tack
In the mechanical testing of seals, a specimen strip exactly 15 mm wide is die-cut perpendicular to the seal and pulled apart in the tensile testing machine at a defined speed. But be careful: anyone who looks only at the bare figure in N/15 mm in the test report often overlooks the most important information!
“Force values alone are not enough – the failure pattern tells the truth.”
That is why, at Innoform, we always document the tear or failure pattern for every seal strength measurement:
- Clean peel (separation of the sealant layer): Desirable for easy-opening packaging; for permanent seals, however, it indicates a sealing temperature that is too low (cold seal).
- Break directly at the seal edge (seal edge failure): A typical sign of excessive sealing temperature or sealing pressure – the sealant layer has been squeezed and weakened at the edge of the jaw.
- Delamination of the laminate: The seal is stronger than the lamination between the individual layers – the film splits within the laminate (an indication of insufficient bond strength or an unsuitable laminating adhesive).
- Elongation / break in the free film strip: The seal is stronger than the base material itself (a true weld seal).
| Test method at Innoform Testservice | Standard / basis | Measured variable & temperature range | Typical practical benefit |
|---|---|---|---|
| Seal strength (strip tensile test) | DIN 55529, ASTM F 88 / F 88M, DIN EN 868-5 Annex D | Maximum force / force curve in N/15 mm (-40 °C to +120 °C) incl. failure pattern | Quality control of finished pouches, medical packaging & trays; testing under deep-freeze or pasteurisation conditions |
| Sealing curves on the laboratory heat sealer | DIN 55529, ASTM F 88 | Seal strength as a function of temperature, time & pressure (e.g. 80 – 220 °C) | Determination of seal initiation temperature (SIT) and optimum sealing window; comparison of new mono-materials with reference films |
| Hot tack test | DIN 55571-2, ASTM F 1921 | Maximum holding force of the still-hot seal in N/15 mm immediately after the jaws open | Indispensable for high-speed VFFS and HFFS flow-wrap machines as well as heavy, free-flowing or frozen products |
| Opening forces of peelable packs | DIN 55409-1 (flexible), DIN 55409-2 (rigid) | Initial peel force and continued peel force in N on the original pack | Practical assessment of opening behaviour (easy opening) from the consumer’s perspective |
| Seal quality of PE sacks & paper | DIN 55529, GKV test sheets I–IV, DIN EN 868-4 | Seal strength, fibre tear & seal quality | Safeguarding heavy-duty sacks, industrial bags and sterilisable paper/film packaging |
Pillar 2: Overview of leak tightness tests and leak detection
A high seal strength in the strip tensile test does not prove that no hair-fine capillary has remained open in the 2-/4-layer gusset area. That is why, within our seal strength & leak tightness testing services, we combine strength testing with targeted leak detection and leak tightness tests:
| Leak tightness / leak test method | Standard / test specification | Detection limit (approx.) | Principle & ideal application |
|---|---|---|---|
| Tracer gas method (forming gas N₂/H₂) | IVLV Information Sheet No. 102 | < 10 µm (gas-tight) | Filling with a hydrogen/nitrogen mixture and highly sensitive H₂ sniffer probe; non-destructive localisation of the smallest gas leaks in MAP and vacuum packs |
| Dye method with methylene blue | DIN 55508-2 | approx. 10 – 20 µm | An alcohol solution with low surface tension creeps into even the finest seal capillaries and gussets and stains defects a high-contrast blue |
| Dye penetration test (rhodamine B / aqueous) | ASTM F 1929 | approx. 15 – 50 µm | International standard (especially pharma/medical) for detecting channels in transparent and opaque seals |
| Penetrating oil test & original product test | In-house method PV036 | approx. 10 – 20 µm | Special test for oily and fatty products and for detecting the finest pores (pinholes) after flex stress (Gelbo Flex) |
| Vacuum chamber / water bath (bubble test) | Standard laboratory method (DIN EN ISO 11607 / ASTM D 3078) | approx. 15 – 30 µm | The sealed pack is submerged under a defined vacuum; escaping gas bubbles immediately reveal the exact location of the leak |
| Light table & copper deposition | DIN EN 546-4, FhG Information Sheet 29 Part 1 | from 20 µm (optical) or micro-pinholes | Testing of aluminium foils and aluminium laminates for pores, flex cracks and corrosion defects |
Practical checklist: How to permanently eliminate complaints caused by poor seals
From our day-to-day consulting work, five specific rules have proven effective in helping film manufacturers, converters and packers drastically reduce their failure rates:
- Specify performance, not just film thicknesses: Make the seal initiation temperature (SIT), the sealing window in °C, the required seal strength in
N/15 mm(including the desired failure mode!) and, for high-speed flow-wrap processes, the minimum hot tack binding requirements in your film specification. - Retain reference samples systematically: Set aside an unprinted or unsealed reference sample from a film batch that has demonstrably run perfectly. If machine problems occur later, a direct laboratory comparison of good and bad samples can clarify within a few days what has changed.
- Test in the laboratory before switching to mono-materials: Do not take new all-PE, all-PP or paper-based laminates onto the production line “flying blind”. A sealing curve and hot tack curve recorded in the laboratory beforehand saves costly machine downtime and tonnes of waste.
- Check sealing jaws regularly by thermography and mechanical testing: As the OFI study already showed, the digital display on the control cabinet often does not match the actual surface temperature of the sealing jaw. Check the temperature profile and pressure distribution regularly (e.g. using carbon paper or pressure-indicating film imprints), especially in the area of the 2-to-4-layer transition.
- Test leak tightness with the right method: Briefly squeezing the pouch by hand or a non-specific water bath test is often not sufficient for MAP and high-barrier packs. For critical products, use dye penetration testing to DIN 55508-2 or the tracer gas method according to IVLV Guideline 102.
Knowledge prevents failure costs: Our relevant Innoform seminars
Good test results only deliver their full benefit when purchasing, quality assurance, packaging development and machine operators speak the same technical language. If you and your team would like to delve deeper into the relationships between polymer structure, sealing technology and test methodology, I recommend our practice-oriented web seminars and courses at Innoform Coaching:
- Leak testing, sealing and processing of barrier film packaging – Barrier Films Part 4 (BVd) (in German): Our specialist seminar covering the difference between leak tightness and permeation, contamination in the seal area, peel systems and modern leak testing methods.
- Fundamentals of Packaging Films – Part G (Sealing layers & sealing properties of PE and PP) and Part C (Describing film properties with test results) (in German): How raw material density, melt flow rate (MFR), coextrusion and test standards govern machinability.
- Mechanical film testing – The tensile test (with live demonstrations from the laboratory) (in German): Everything about specimen preparation, grips, seal strength, bond strength and failure pattern analysis.
- Packing in flexible packaging (FFS systems & modified atmosphere packaging MAP) (in German): The direct interaction of film, forming shoulder, sealing tools and modified atmosphere right at the packaging machine.
Frequently asked questions on seal strength and leak testing (FAQ)
Why does a package sometimes leak despite high seal strength in N/15 mm?
Seal strength according to DIN 55529 or ASTM F 88 measures the mechanical holding force on a 15 mm wide strip of the cooled seal. Leaks, however, often occur at isolated points – for example through a fine capillary (10–30 µm) at the 2-to-4-layer transition (side fold/gusset), through individual product particles in the seal, or through brief opening of the still-hot seal due to insufficient hot seal strength (hot tack). Strength testing should therefore always be supplemented by targeted leak testing (e.g. methylene blue test to DIN 55508-2 or tracer gas test).
According to studies, how many modified atmosphere packs (MAP) in retail are defective?
In the well-known market study by the Austrian Research Institute for Chemistry and Technology (OFI) in Vienna covering more than 1,600 MAP packs in the German-speaking region, only 56 % had an optimal modified atmosphere; around one third to 44 % (and almost 50 % in a German retail sample of 386 packs) showed defects. Supplementary studies (WRAP, Fraunhofer IVV / IVLV Guideline 114) show that in 58 % of defective packs a contaminated seal is the main cause. In current practice, it can be assumed that 70 to 80 % of all genuine package leaks are located in or directly adjacent to the seal.
Which test method detects even the smallest micro-leaks in seals?
For directly visualising very fine channels in the seal from approx. 10–20 µm, dye penetration testing with methylene blue solution to DIN 55508-2 (or ASTM F 1929 with aqueous dye solution) is ideally suited. If closed packs are to be tested non-destructively for gas tightness (defects < 10 µm), the tracer gas method using forming gas (hydrogen/nitrogen) and a sensitive hydrogen sensor in accordance with IVLV Guideline No. 102 is the method of choice.
When should a hot tack test be carried out in addition to the sealing curve?
A hot tack test according to DIN 55571-2 or ASTM F 1921 is indispensable whenever the seal is subjected to mechanical stress while it is still hot and not yet fully cooled. This applies above all to high-speed vertical and horizontal form-fill-seal machines (v-FFS / h-FFS), heavy or sharp-edged products, and the switch from conventional PET/PE laminates to mono-materials (PE, PP) or barrier papers.
My conclusion: when damage occurs, let the analysis do the talking!
Leaking packs are not an unavoidable fate – and certainly no reason for weeks of finger-pointing between film supplier and packer. Whether a seal fails because of product contamination, a sealing window that is too narrow with the new mono-material, insufficient hot tack or an open gusset at the 2-/4-layer transition can now be clarified in the laboratory quickly, objectively and in compliance with standards.
My advice from practice is therefore: Specify rather than speculate. And if things do get stuck on the line, or packs start drawing air at retail: don’t blindly adjust the sealing temperature – send your good and bad samples to our laboratory in Oldenburg instead. We test seal strength and leak tightness under accreditation, all from a single source, and deliver results that let you get production running reliably again straight away.
Yours, Karsten Schröder
Innoform Testservice – your accredited test laboratory for flexible packaging
Sources and references (technical literature, studies & test standards)
- Österreichisches Forschungsinstitut für Chemie und Technik (OFI), Vienna; Washüttl, M., Tacker, M., Tauschitz, B.: Market studies on the quality of food packed under modified atmosphere (MAP) in German-speaking retail (examination of more than 1,600 MAP packs in Germany, Austria and Switzerland and 386 packs in German food retail).
- WRAP (Waste & Resources Action Programme), UK; Dudbridge, M., Turner, R. (University of Lincoln): Seal Integrity and the Impact on Food Waste – study of leakage causes and contamination in the seal area.
- Industrievereinigung für Lebensmitteltechnologie und Verpackung e. V. (IVLV) / Fraunhofer Institute for Process Engineering and Packaging (IVV), Freising (in cooperation with Universiteit Hasselt & KU Leuven): IVLV Technical Leaflet No. 114 (research project EVOCOSEAL – influence of product contamination in the seal area on seal quality) and IVLV Technical Leaflet No. 102 (tracer gas method for leak testing of packaging using forming gas N₂/H₂).
- DIN 55529: Packaging – Determination of the seal strength of seals made from flexible packaging materials (strip tensile test and assessment of the failure pattern).
- ASTM F 88 / F 88M: Standard Test Method for Seal Strength of Flexible Barrier Materials.
- DIN 55571-2 and ASTM F 1921 / F 1921M: Determination of hot seal strength (hot tack) of heat-sealable thermoplastic polymers and flexible barrier materials immediately after the sealing process.
- DIN 55508-2: Testing of packaging – Leak testing of flexible packaging, Part 2: Dye method (methylene blue solution); supplemented by DIN EN 868-5 and ASTM F 1929 (Standard Test Method for Detecting Seal Leaks in Porous Medical Packaging by Dye Penetration).
- DIN 55409-1 and DIN 55409-2: Testing of packaging – Determination of the opening forces of peelable packaging (Part 1: Flexible packaging; Part 2: Rigid packaging/trays).
- ASTM D 3078: Standard Test Method for Determination of Leaks in Flexible Packaging by Bubble Emission (vacuum chamber water bath test) and DIN EN ISO 11607-1.
- DIN EN 546-4 and Fraunhofer Technical Leaflet No. 29 Sheet 1: Testing of aluminium foils and aluminium composite films for pores (pinholes) and flex cracks using a light table and electrolytic copper deposition.
- Schröder, K.: Seminar documents “Leak Testing, Sealing and Processing of Barrier Film Packaging (Barrier Films Part 4 – BVd)” and “Fundamentals of Packaging Films”, Innoform Coaching / Innoform Testservice, Oldenburg.
